Limitaciones del acero para herramientas H13: modos de falla y cómo evitarlos
El acero para herramientas H13 es uno de los aceros para herramientas de trabajo en caliente más confiables, con la dureza en caliente, tenacidad y resistencia a la fatiga térmica necesarias para moldes de fundición a presión, troqueles de forja en caliente y herramientas de extrusión. Aun así, tiene límites reales.
Cuando esos límites se ignoran en el diseño, mecanizado, tratamiento térmico, soldadura, rectificado o selección de material, los troqueles fallan prematuramente y los costos aumentan. Esta guía explica en qué puntos el H13 presenta deficiencias y cómo prevenir una falla prematura.
Suministro de acero para herramientas H13 para herramientas de trabajo en caliente confiables
Aobo Steel suministra H13 convencional y H13 ESR en forma forjada y laminada, principalmente en condición recocida para mecanizado antes del tratamiento térmico. La calidad adecuada del material, el tratamiento térmico y el control del proceso son esenciales para prevenir la falla prematura de los troqueles de H13.
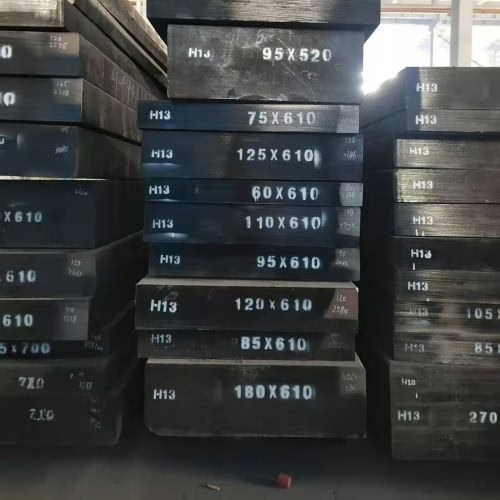
H13 | 1.2344 | SKD61
Acero para herramientas de trabajo en caliente para moldes de fundición a presión, troqueles de forja en caliente, herramientas de extrusión, cuchillas de corte en caliente, pasadores de núcleo, insertos de troquel y componentes de molde que requieren tenacidad y resistencia al agrietamiento térmico.
Quick Guide to H13 Limitations
| Limitation or Failure Mode | Why It Happens | How to Avoid It |
|---|---|---|
| Corrosion and pitting | H13 has about 5% chromium, so it is not stainless. | Use coatings, nitriding, controlled storage, or a corrosion-resistant grade. |
| Softening at excessive temperature | Strength drops sharply above about 650°C. | Keep service temperature within the rated hot-work range or choose a higher-temperature grade. |
| Mecanizado difícil | H13 toughness increases tool wear, especially after hardening. | Machine in annealed condition when possible and use proper carbide or PCBN tooling for hard machining. |
| Weld cracking | Fast cooling can form brittle untempered martensite in the heat-affected zone. | Use preheat, matching filler, and post-weld heat treatment. |
| Grietas de molienda | Local overheating creates brittle re-hardened layers or thermal stress. | Use correct wheel selection, controlled passes, and well-directed coolant. |
| Heat-treatment defects | Decarburization, distortion, cracking, and retained austenite come from poor process control. | Control furnace atmosphere, heating rate, quenching rate, and tempering cycles. |
| In-service cracking and wear | Thermal fatigue, stress risers, segregation, scale abrasion, and galling drive failure. | Improve design radii, heat treatment, cooling practice, surface finish, and material quality. |
Is H13 Tool Steel Corrosion-Resistant?
No. H13 contains about 5% chromium, but it is not stainless and offers little corrosion resistance. Reliable rust prevention requires a chromium content of about 11-12%. In moist environments, cooling water, or corrosive operating conditions, H13 surfaces can pit, and those pits become stress concentration points that initiate cracks.
Treat corrosion as a design issue, not a property you can rely on. Surface treatments such as nitriding or coatings, along with controlled storage and operating environments, are practical defenses. Pitting, left unchecked, can shorten die life before mechanical wear does.
At What Temperature Does H13 Lose Strength and Toughness?
H13 holds up well at elevated temperature, but strength drops sharply above about 650°C (1202°F) as the structure begins to transform. Run a die beyond its rated range, and it softens, increasing the risk of failure.
Toughness is also set in tempering. The temperature window that produces that low toughness state, and the other embrittlement mechanisms that share it, are listed with their remedies on the página de tipos de fragilización del acero. Tempering near 500°C (930°F) can leave H13 in a high-hardness, low-toughness state known as temper brittleness. Too high an austenitizing temperature coarsens the grain and embrittles grain boundaries.
The fix is tight control of austenitizing and tempering, usually two or three tempering cycles, to balance hardness and toughness. For the full procedure, see the Guía de tratamiento térmico del acero para herramientas H13.
How Hard Is H13 to Machine?
H13 is moderately difficult to machine. Its machinability rating is about 70 compared with 1% carbon steel at 100, and its toughness accelerates tool wear and raises costs. Machining is far easier in the annealed condition than after hardening.
Where hardened H13 must be cut, around 52-55 HRC, coated solid carbide or PCBN tooling, low depths of cut of 0.05-0.3 mm, and feeds of 0.05-0.2 mm/rev help keep pressure and heat under control. Surface finishes around 0.14-0.48 µm are achievable with proper setup. For detailed parameters, see Maquinabilidad del acero para herramientas H13.
Can H13 Tool Steel Be Welded?
Yes, but it is high-risk and prone to cracking. As a high-hardenability alloy, H13 forms brittle untempered martensite in the heat-affected zone on fast cooling, which drives hydrogen-induced cold cracking. That cracking can appear days or weeks after welding, past the first inspection.
Successful repair requires a preheat of 100-200°C, a filler matched to the H13 composition and hardness, and post-weld heat treatment to transform retained austenite and relieve stress. Skip any one of these, and the weld zone becomes the next crack origin. For the full method and limits, see Can H13 Tool Steel Be Welded?.
Why Do Grinding Cracks Form on H13?
Grinding cracks come from local overheating. When a pass heats the surface faster than the bulk can absorb, the surface either re-hardens into a brittle white layer at 65-70 HRC or softens due to local tempering. The resulting thermal stress opens fine cracks.
These microcracks are often invisible but deepen with abusive passes and become prime fatigue initiation sites. Correct wheel selection, controlled speeds, and sufficient, well-directed coolant prevent the damage. Treat grinding as a finishing step that can quietly destroy an otherwise sound die.
What Goes Wrong During H13 Heat Treatment?
Heat treatment is where most H13 dies are made or lost. Four failure modes dominate: decarburization leaves a soft, low-wear surface skin; distortion and cracking follow uneven heating or quenching, especially in complex sections; and retained austenite stays soft and unstable, then transforms later and embrittles the die.
Each one traces back to atmosphere control and heating or cooling rate rather than to the grade itself. These are process faults, not material limits, so the defense is procedure. The full hardening, quenching, and tempering controls are covered in the Guía de tratamiento térmico del acero para herramientas H13.
What Are the Most Common H13 Failure Modes in Service?
Thermal fatigue
Heat checking is the most common hot-work die failure. Repeated heat-and-cool cycles create fine surface cracks.
Gross cracking
Large fractures often start at stress risers and are worsened by coarse grain, segregation, or excess retained austenite.
Tener puesto
Forging dies often fail by abrasion from scale and hard particles, plus adhesive galling at high temperature.
Thermal fatigue, or heat checking, is especially common in die casting. Molten aluminum forced into those cracks under pressure worsens part extraction and surface quality. Gross cracking is a large, deep fracture caused by combined mechanical and thermal stresses at stress risers, such as small radii. Wear dominates many forging applications and can account for a large share of die failures.
When Should You Not Use H13?
Choose a different grade when the job is dominated by corrosion, very high abrasive wear, or service temperatures past H13’s softening range. H13 is a hot-work workhorse, not a stainless steel or a high-wear cold-work steel.
For wet or chemically aggressive environments, a corrosion-resistant grade is better suited. For heavy abrasive wear at lower temperatures, a high-carbon high-chromium cold-work steel such as D2 holds an edge longer. Matching the grade to the dominant failure mode is cheaper than operating H13 outside its strength range.
Does Material Quality Affect H13 Failure?
Yes, and it is often the hidden cause. Many premature H13 failures trace back to the steel itself rather than the grade specification. Cleanliness, hardenability control, and low segregation decide how well a die resists cracking and heat checking, and two bars to the same H13 chemistry can behave differently in service.
Inclusions and carbide segregation act as crack initiation sites, and a non-homogeneous structure lowers toughness where stress concentrates. ESR H13 reduces inclusions and segregation, which is why it is the common upgrade for demanding die-casting and extrusion dies. Annealed-condition stock also machines more predictably and carries less residual stress into the hardening process. For when the upgrade is worth it, see ¿Cuándo elegir el acero para herramientas ESR H13?.
Bottom line: most H13 failures are not caused by choosing a bad grade. They come from using H13 outside its natural range, poor heat treatment, uncontrolled finishing, risky welding, or material quality that is not matched to the application.
Need H13 Matched to the Failure Risk?
Send your application, tool size, working temperature, hardness target, and failure concern. Aobo Steel can help confirm whether conventional H13 or ESR H13 is the better supply route.