
General Properties of Tool Steels
Reference table of the principal AISI tool steel grades, covering wear resistance, toughness, hot hardness, usual working hardness, depth of hardening, grain size and hardness after hardening. Ratings are relative comparisons on a 1 (low) to 9 (high) scale and are a practical starting point when selecting a grade for a given tooling application.
| Grade | Wear (b) | Toughness (c) | Hot hardness | Working hardness, HRC | Depth (d) | Grain size (Shepherd) | Surface HRC | Core HRC |
|---|---|---|---|---|---|---|---|---|
| Molybdenum high-speed steels | ||||||||
| M1 | 7 | 3 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M2 | 7 | 3 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M3, class 1 | 8 | 3 | 8 | 63–66 | D | 9½ | 64–66 | 64–66 |
| M3, class 2 | 8 | 3 | 8 | 63–66 | D | 9½ | 64–66 | 64–66 |
| M4 | 9 | 3 | 8 | 63–66 | D | 9½ | 65–67 | 65–67 |
| M7 | 8 | 3 | 8 | 63–66 | D | 9½ | 64–66 | 64–66 |
| M10 | 7 | 3 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M30 | 7 | 2 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M33 | 8 | 1 | 9 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M34 | 8 | 1 | 9 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M35 | 7 | 2 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M36 | 7 | 1 | 9 | 63–65 | D | 9½ | 64–66 | 64–66 |
| M41 | 8 | 1 | 9 | 66–70 | D | 9½ | 63–65 | 63–65 |
| M42 | 8 | 1 | 9 | 66–70 | D | 9½ | 63–65 | 63–65 |
| M43 | 8 | 1 | 9 | 66–70 | D | 9½ | 63–65 | 63–65 |
| M44 | 8 | 1 | 9 | 66–70 | D | 9½ | 63–65 | 63–65 |
| M46 | 8 | 1 | 9 | 66–69 | D | 9½ | 63–65 | 63–65 |
| M47 | 8 | 1 | 9 | 66–70 | D | 9½ | 63–65 | 63–65 |
| Intermediate high-speed steels | ||||||||
| M50 | 6 | 3 | 6 | 61–63 | D | 8½ | 63–65 | 63–65 |
| M52 | 6 | 3 | 6 | 62–64 | D | 8½ | 63–65 | 63–65 |
| Tungsten high-speed steels | ||||||||
| T1 | 7 | 3 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| T2 | 8 | 3 | 8 | 63–66 | D | 9½ | 65–67 | 65–67 |
| T4 | 7 | 2 | 8 | 63–65 | D | 9½ | 63–66 | 63–66 |
| T5 | 7 | 1 | 9 | 63–65 | D | 9½ | 64–66 | 64–66 |
| T6 | 8 | 1 | 9 | 63–65 | D | 9½ | 64–66 | 64–66 |
| T8 | 8 | 2 | 8 | 63–65 | D | 9½ | 64–66 | 64–66 |
| T15 | 9 | 1 | 9 | 64–68 | D | 9½ | 65–68 | 65–68 |
| Chromium hot-work steels | ||||||||
| H10 | 3 | 9 | 6 | 39–56 | D | 8 | 52–59 | 52–59 |
| H11 | 3 | 9 | 6 | 38–55 | D | 8 | 53–55 | 53–55 |
| H12 | 3 | 9 | 6 | 38–55 | D | 8 | 53–55 | 53–55 |
| H13 | 3 | 9 | 6 | 40–53 | D | 8 | 51–54 | 51–54 |
| H14 | 4 | 6 | 7 | 40–54 | D | 8 | 53–57 | 53–56 |
| H19 | 5 | 6 | 7 | 40–55 | D | 8½ | 48–57 | 48–57 |
| Tungsten hot-work steels | ||||||||
| H21 | 4 | 6 | 8 | 40–55 | D | 9 | 45–63 | 45–63 |
| H22 | 5 | 5 | 8 | 36–54 | D | 9 | 48–56 | 48–56 |
| H23 | 5 | 5 | 8 | 38–48 | D | 7 | 34–40 | 34–40 |
| H24 | 5 | 5 | 8 | 40–55 | D | 9 | 52–56 | 52–56 |
| H25 | 4 | 6 | 8 | 35–45 | D | 9 | 33–46 | 33–46 |
| H26 | 6 | 4 | 8 | 50–58 | D | 9 | 51–59 | 51–59 |
| Molybdenum hot-work steels | ||||||||
| H42 | 6 | 4 | 7 | 45–62 | D | 8½ | 54–62 | 54–62 |
| Air-hardening, medium-alloy, cold-work steels | ||||||||
| A2 | 6 | 4 | 5 | 57–62 | D | 8½ | 63–65 | 63–65 |
| A3 | 7 | 3 | 5 | 58–63 | D | 8½ | 63–65 | 63–65 |
| A4 | 5 | 4 | 4 | 54–62 | D | 8½ | 61–63 | 61–63 |
| A5 | 5 | 4 | 4 | 54–60 | D | 8½ | 60–62 | 60–62 |
| A6 | 4 | 5 | 4 | 54–60 | D | 8½ | 60–62 | 60–62 |
| A7 | 9 | 1 | 6 | 58–66 | D | 8½ | 64–66 | 64–66 |
| A8 | 4 | 8 | 6 | 48–57 | D | 8 | 60–62 | 60–62 |
| A9 | 4 | 8 | 6 | 40–56 | D | 8 | 55–57 | 55–57 |
| A10 | 3 | 3 | 3 | 55–62 | D | 8 | 60–63 | 60–63 |
| High-carbon, high-chromium, cold-work steels | ||||||||
| D2 | 8 | 2 | 6 | 58–64 | D | 7½ | 61–64 | 61–64 |
| D3 | 8 | 1 | 6 | 58–64 | D | 7½ | 64–66 | 64–66 |
| D4 | 8 | 1 | 6 | 58–64 | D | 7½ | 64–66 | 64–66 |
| D5 | 8 | 2 | 7 | 58–63 | D | 7½ | 61–64 | 61–64 |
| D7 | 9 | 1 | 6 | 58–66 | D | 7½ | 64–68 | 64–68 |
| Oil-hardening cold-work steels | ||||||||
| O1 | 4 | 3 | 3 | 57–62 | M | 9 | 61–64 | 59–61 |
| O2 | 4 | 3 | 3 | 57–62 | M | 9 | 61–64 | 59–61 |
| O6 | 3 | 3 | 2 | 58–63 | M | 9 | 65–67 | 50–55 |
| O7 | 5 | 3 | 3 | 58–64 | M | 9 | 61–64 | 59–61 |
| Shock-resisting steels | ||||||||
| S1 | 4 | 8 | 5 | 50–58 | M | 8 | 55–58 | 55–58 |
| S2 | 2 | 8 | 2 | 50–60 | M | 8 | 61–63 | 56–60 |
| S5 | 2 | 8 | 3 | 50–60 | M | 9 | 61–63 | 58–62 |
| S6 | 2 | 8 | 3 | 50–56 | M | 8 | 56–58 | 56–58 |
| S7 | 3 | 8 | 5 | 47–57 | D | 8 | 59–61 | 59–61 |
| Low-alloy special-purpose steels | ||||||||
| L2 | 1 | 7 | 2 | 45–62 | M | 8½ | 56–62 | 54–58 |
| L6 | 3 | 6 | 2 | 45–62 | M | 8 | 58–63 | 58–62 |
| Low-carbon mold steels | ||||||||
| For hubbed and/or carburized cavities | ||||||||
| P2 (e) | 1(e) | 9 | 2(e) | 58–64 (e) | S | … | 62–65 (a) | 15–21 |
| P3 (e) | 1(e) | 9 | 2(e) | 58–64 (e) | S | … | 62–64 (a) | 15–21 |
| P4 (e) | 1(e) | 9 | 4(e) | 58–64 (e) | M | … | 62–65 (a) | 33–35 |
| P5 (e) | 1(e) | 9 | 2(e) | 50–64 (e) | S | … | 62–65 (a) | 20–25 |
| P6 (e) | 1(e) | 9 | 3(e) | 58–61 (e) | M | … | 60–62 (a) | 35–37 |
| For machined cavities | ||||||||
| P20 (e) | 1(e) | 8 | 2(e) | 30–50 | M | 7½ | 52–54 | 45–50 |
| P21 | 1 | 8 | 4 | 36–39 (e) | D | … | 22–26 | 22–26 |
| Water-hardening tool steels | ||||||||
| W1 | 2–4 | 3–7 | 1 | 58–65 | S | 9 | 65–67 | 38–43 |
| W2 | 2–4 | 3–7 | 1 | 58–65 | S | 9 | 65–67 | 38–43 |
| W5 | 3–4 | 3–7 | 1 | 58–65 | S | 9 | 65–67 | 38–43 |
Notes & References
- (a) Rating range from 1 (low) to 9 (high).
- (b) Wear resistance increases with increasing carbon content.
- (c) Toughness decreases with increasing carbon content and depth of hardening.
- (d) S, shallow; M, medium; and D, deep.
- (e) After carburizing.
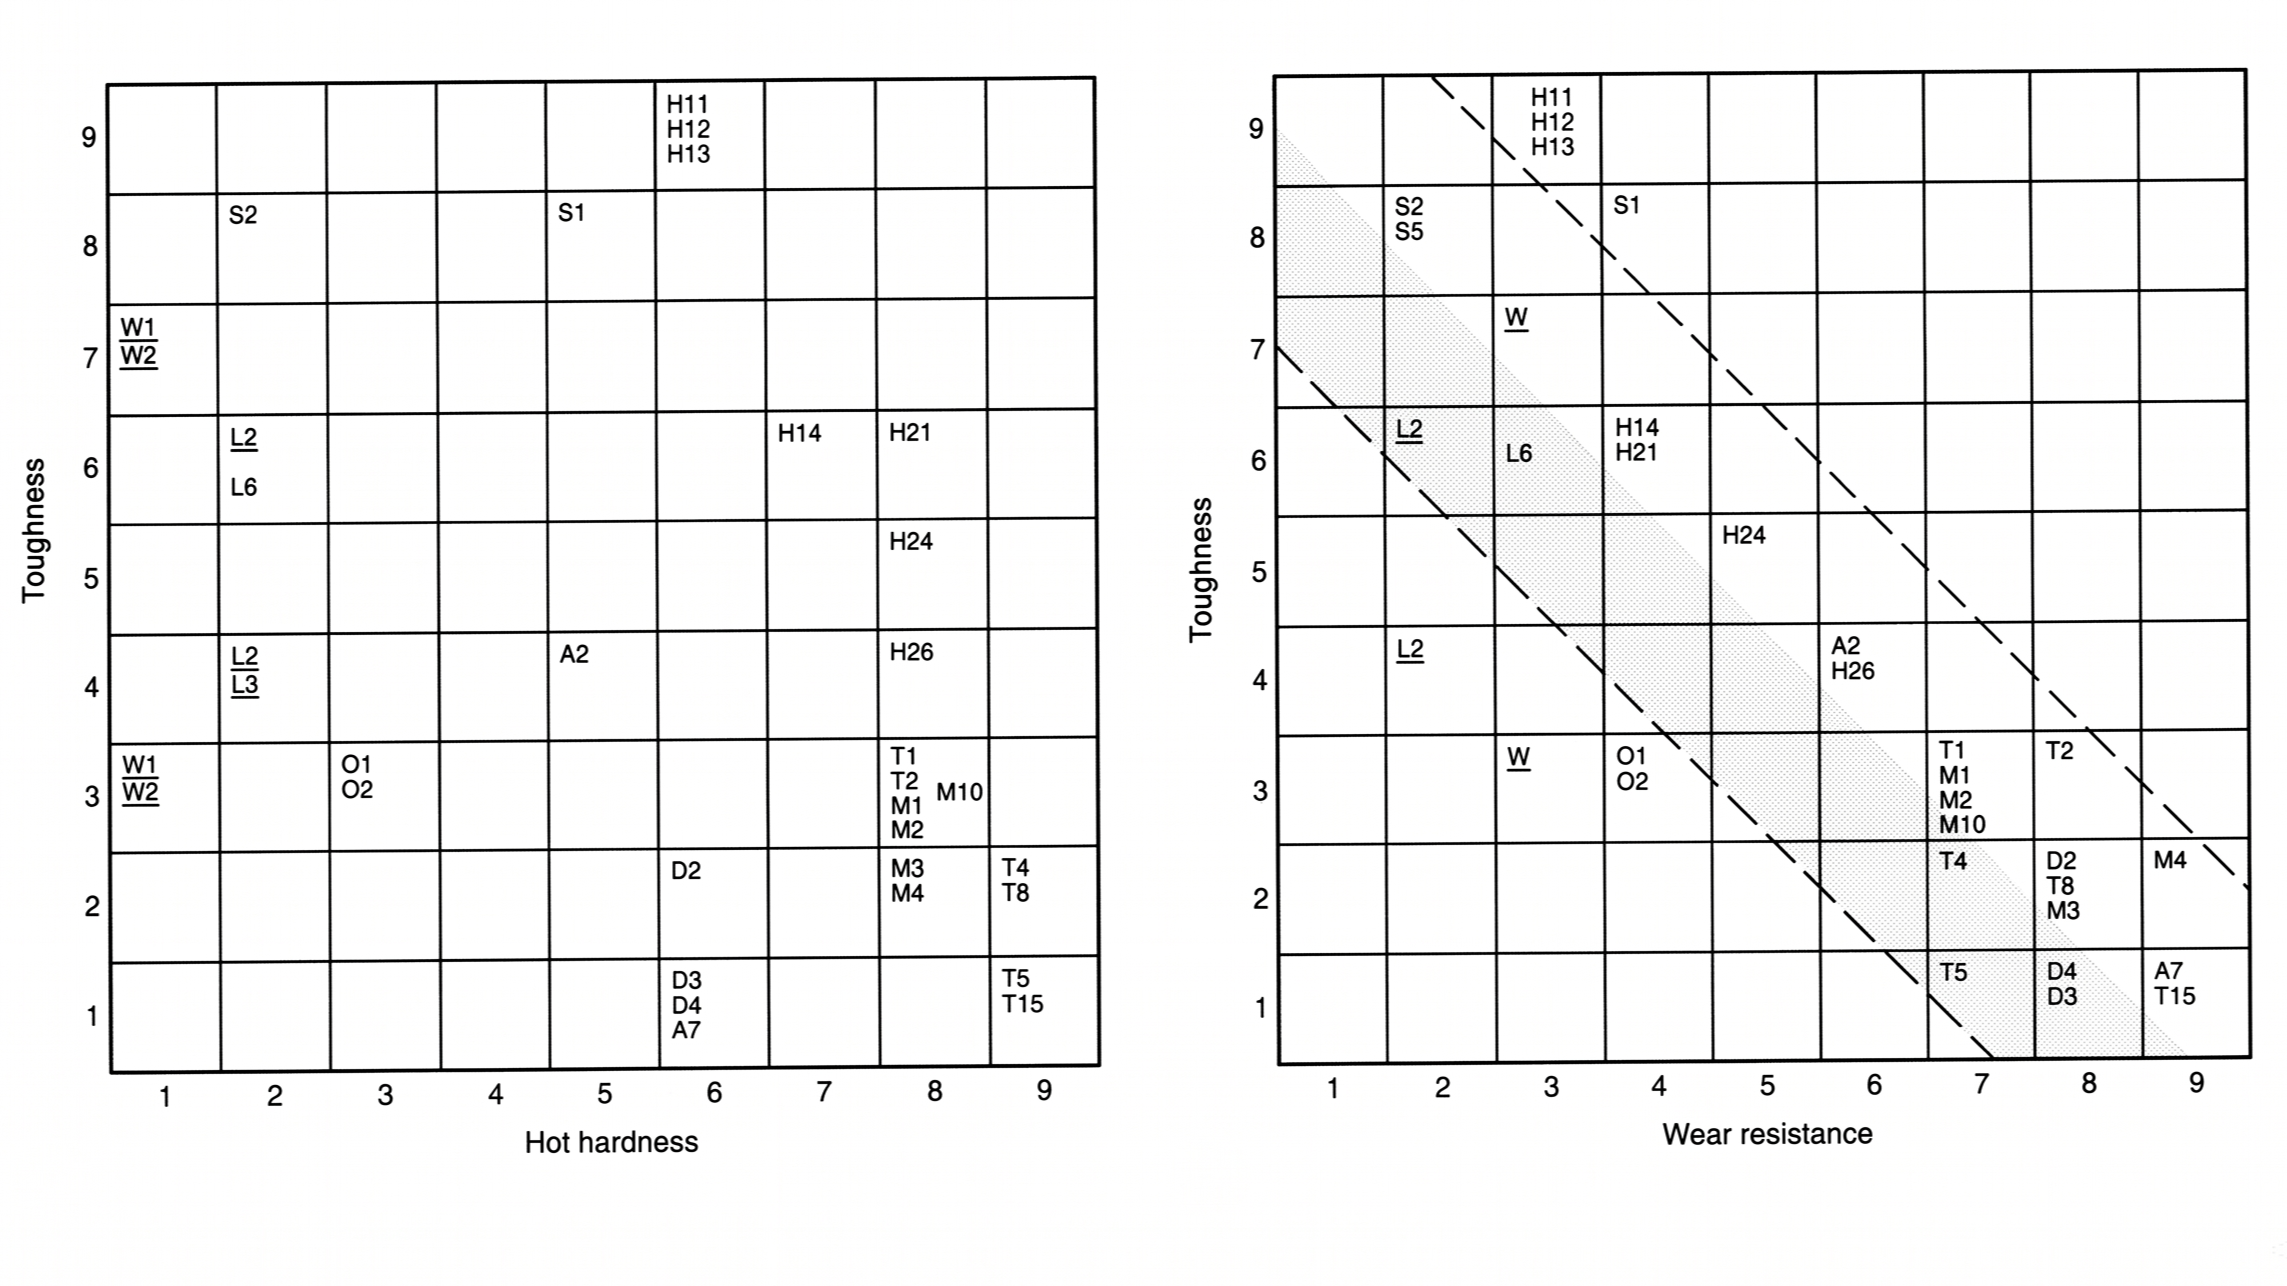
Elastic modulus of tool steels
For all practical purposes, the modulus of elasticity of all tool steels in all conditions is about 210 GPa (30 × 106 psi) at room temperature. It decreases uniformly to about 185 GPa (27 × 106 psi) at 260 °C (500 °F) and about 150 GPa (22 × 106 psi) at 540 °C (1000 °F).
Wear resistance
Wear resistance increases with carbon content. At a given hardness, however, it may vary widely depending on the wear mechanism and heat treatment used. Steels with similar hardness can behave very differently under identical wear conditions. The grades that resist wear best are also the hardest to machine, and the machinability rating chart puts a number on that trade-off.
Toughness & testing
At maximum hardness, most tool steels are brittle, so tensile testing rarely gives reliable strength values. Compression, bending and torsion tests are more useful; torsion impact testing gives reproducible data on the effect of composition and heat treatment, particularly for drills and tools loaded in torsion. Where toughness and wear resistance pull in opposite directions, selection by application is the faster route to a grade.
Supply Scope & Technical Reference Note
Aobo Steel supplies tool steel in round bar and plate form, in annealed condition. Hardening, quenching and tempering are performed by the customer’s heat-treatment facility. The tool steel heat treatment guide covers austenitizing temperatures, soak times and tempering windows for these grades.
The property ratings and hardness data in this reference are relative comparisons compiled from ASM Handbook, Volume 1, Table 13. Actual performance depends on heat treatment, section size, tool geometry and service conditions. Always verify final properties and heat-treatment procedures with your heat-treatment facility.
Related reference pages
Tool steel composition chart · Tool steel hot hardness chart · Hardening and tempering temperatures · Machinability ratings · Selection by application · Grade comparison and equivalents · Hardness conversion calculator · Tool steel heat treatment guide · Tool steel thermal conductivity chart
Source: ASM Handbook, Volume 1 — Properties and Selection: Irons, Steels, and High-Performance Alloys, Table 13 “General properties of tool steels” (data for grades marked “e” after carburizing). Reference data for comparison — verify final heat treatment with the grade supplier.