
S7 Tool Steel Heat Treatment Guide
S7 tool steel is typically heat-treated by preheating to 1200–1250°F (649–677°C), austenitizing at about 1725°F (940°C), air quenching for sections up to about 2.5 in. (63.5 mm), and applying immediate double tempering. For most cold-work tooling, S7 is commonly tempered at 400–500°F (204–260°C), producing a typical working hardness of about 56–58 HRC.

Aobo Steel supplies S7 tool steel in the annealed condition, ready for your machining and in-house heat treatment. Check the available sizes and stock, or send your requirement for a quote. Size range, tolerances, minimum order and lead times are set out on our tool steel supply capability page.
S7 Tool Steel Heat Treatment Quick Guide
| Process Phase | Temperature | Soak Time | Cooling Method |
|---|---|---|---|
| Annealing | 815–870 °C | 1–1.5 hr/in | Furnace cool to 482 °C, then air cool |
| Stress Relieving | 649–677 °C | 1–2 hr/in | Furnace cool preferred |
| Preheating | 649–704 °C | Until uniform | — |
| Austenitizing | 940–982 °C | Controlled by section size | Air or oil depending on section size |
| Quenching | — | — | Air ≤63.5 mm; oil or flash oil >63.5 mm |
| Tempering | 204–538 °C | 2 hr/in, twice | Air cool between cycles |
Section size strongly affects the quenching method and final hardness. Thin and medium sections can normally achieve full hardness by air cooling, while heavier sections may require faster cooling to avoid low core hardness.
Step-by-Step S7 Tool Steel Heat Treatment Process
1. Preheating
Protect S7 tool steel from decarburization during heating. Use a controlled-atmosphere furnace, a vacuum furnace, a neutral salt bath, or sealed stainless-steel foil.
Heat uniformly to 1200–1250 °F (649–677 °C) and hold until the entire cross-section reaches the temperature. For small sections, a 10–15 minute soak after temperature equalization is usually sufficient.
Preheating reduces thermal shock, improves temperature uniformity, and lowers the risk of cracking during the final rise to austenitizing temperature.
2. Austenitizing
Raise the temperature to about 1725 °F (940 °C). Timing should begin only after the part has reached its full temperature.
Soak time must be controlled carefully. Excessive temperature or soaking can cause grain coarsening, retained austenite, lower toughness, and dimensional instability.
| Section Thickness | Recommended Soak Time |
|---|---|
| 1/8 in. / 3.2 mm | 30 min |
| 1/4 in. / 6.4 mm | 40 min |
| 1/2 in. / 12.7 mm | 45–50 min |
| 3/4 in. / 19 mm | 50–55 min |
| ≥1 in. / 25 mm | About 1 hr/in |
3. Quenching
For sections up to 2.5 in. (about 63.5 mm), use still-air cooling. Cool the part to approximately 150 °F (65 °C) before tempering.
For sections above 2.5 in., use a faster cooling method. A flash oil quench is commonly used: immerse and agitate until the visible red heat disappears, then remove the part and air cool to about 150 °F.
Air quenching provides better dimensional control, while oil-based cooling helps larger sections achieve sufficient hardness throughout the cross-section.
4. Tempering
Begin tempering immediately when the part cools to about 150 °F (65 °C).
S7 requires double tempering. Each tempering cycle should be held for 2 hours per inch of section thickness, followed by full air cooling to room temperature before the second cycle.
For most cold-work tooling, temper at 400–500 °F (204–260 °C). This typically produces a working hardness around 56–58 HRC.
For hot-work or elevated-temperature applications, temper at 900–1000 °F (482–538 °C) to improve thermal stability.
Low-temperature tempering below 400 °F may increase hardness but also increases the risk of brittleness and is not recommended for standard industrial applications unless maximum hardness is the primary priority and any loss of toughness is acceptable.
S7 Tool Steel Annealing and Stress Relieving
1. Annealing
We supply S7 tool steel in the annealed condition. Re-annealing is usually required only when restoring machinability after hardening or when reworking tools.
Annealing should be performed in a controlled atmosphere, vacuum furnace, or neutral-salt environment to prevent decarburization.
Recommended annealing practice:
| Item | Recommendation |
|---|---|
| Temperature | 815–870 °C, typically around 843 °C |
| Soak time | About 1.5 hr/in |
| Cooling | Furnace cool at ≤14 °C/hr to 482 °C, then air cool |
| Final hardness | Normally not above about 230 HB |
Proper annealing improves machinability and prepares the steel for subsequent hardening.
2. Stress Relieving
Stress relieving is recommended after heavy rough machining, EDM, welding, or when working with complex geometries and uneven sections.
It is not mandatory for every part, but it becomes important when residual stress may cause distortion or cracking during hardening.
Recommended stress-relieving practice:
| Item | Recommendation |
|---|---|
| Temperature | 649–677 °C |
| Soak time | 1–2 hr/in |
| Cooling | Furnace cooling preferred |
Uniform cooling is important. Uneven cooling can introduce new thermal stresses and reduce the benefit of stress relieving.
S7 Tool Steel Hardness After Heat Treatment
The final hardness of S7 tool steel depends mainly on the austenitizing temperature, quenching method, section size, and tempering temperature. Because S7 is selected for shock resistance, heat treatment should not focus only on maximum hardness. The practical target is a stable balance between Rockwell hardness, toughness, and resistance to cracking.
After proper hardening, S7 can reach about 58–64 HRC in the as-quenched condition. However, as-quenched S7 is too brittle for normal tooling use and should be tempered immediately after quenching. For most cold-work tooling, the typical working hardness after tempering is about 56–58 HRC.
| Tempering Temperature | Approximate Hardness | Practical Meaning |
|---|---|---|
| As-quenched, before tempering | 58–64 HRC | Maximum hardness, but too brittle for service. Temper immediately after quenching. |
| 400–500 °F / 204–260 °C | 56–58 HRC | Common cold-work range for punches, dies, shear blades, and shock-loaded tools. |
| Around 450 °F / 230 °C | About 58 HRC | Practical general-purpose range when both wear resistance and impact toughness are required. |
| 500–900 °F / 260–482 °C | About 54–56 HRC | Stable hardness range with better toughness than lower tempering temperatures. |
| 900–1000 °F / 482–538 °C | About 48–52 HRC | Used for hot-work or elevated-temperature applications where thermal stability is more important than maximum hardness. |
| 1050–1150 °F / 565–620 °C | About 45 HRC | High tempering range with significant softening. Used only when lower hardness is acceptable. |
For cold-work applications, S7 is commonly tempered at 400–500 °F to reach about 56–58 HRC. This range is suitable when the tool must resist impact, chipping, and moderate wear simultaneously.
For hot-work or elevated-temperature service, S7 is usually tempered at 900–1000 °F. The hardness is lower, but the steel is better suited for applications where thermal stability and resistance to softening are more important than maximum Rockwell hardness.
Tempering below 400 °F is usually not recommended for standard industrial tooling. It may maintain higher hardness, but it also increases the risk of brittleness and cracking. S7 tools should also be double-tempered, with full cooling to room temperature between tempering cycles, to reduce internal stresses and improve the reliability of the final hardness.
The correct hardness should always be selected according to the tool’s failure mode. If wear is the main problem, the lower tempering range may be suitable. If cracking, chipping, or impact failure is the main problem, a slightly lower hardness with better toughness is usually safer than chasing maximum hardness.
S7 Tool Steel Heat Treatment by Application
S7 heat treatment should be adjusted according to the tool’s working condition. The main variable is usually the tempering temperature.
| Application | Tempering Range | Typical Hardness | Main Priority |
|---|---|---|---|
| Cold-work tooling, dies, punches, shear blades | 400–500 °F / 204–260 °C | 56–58 HRC | Wear and toughness balance |
| Cold-work tooling with maximum hardness focus | 345–400 °F / 175–204 °C | Higher hardness | Maximum wear resistance, lower toughness |
| Hot-work or plastic molding tools | 900–1000 °F / 482–538 °C | 48–52 HRC | Thermal stability |
| Shock-dominant tools | 700–750 °F / 370–400 °C | Moderate hardness | Fracture resistance |
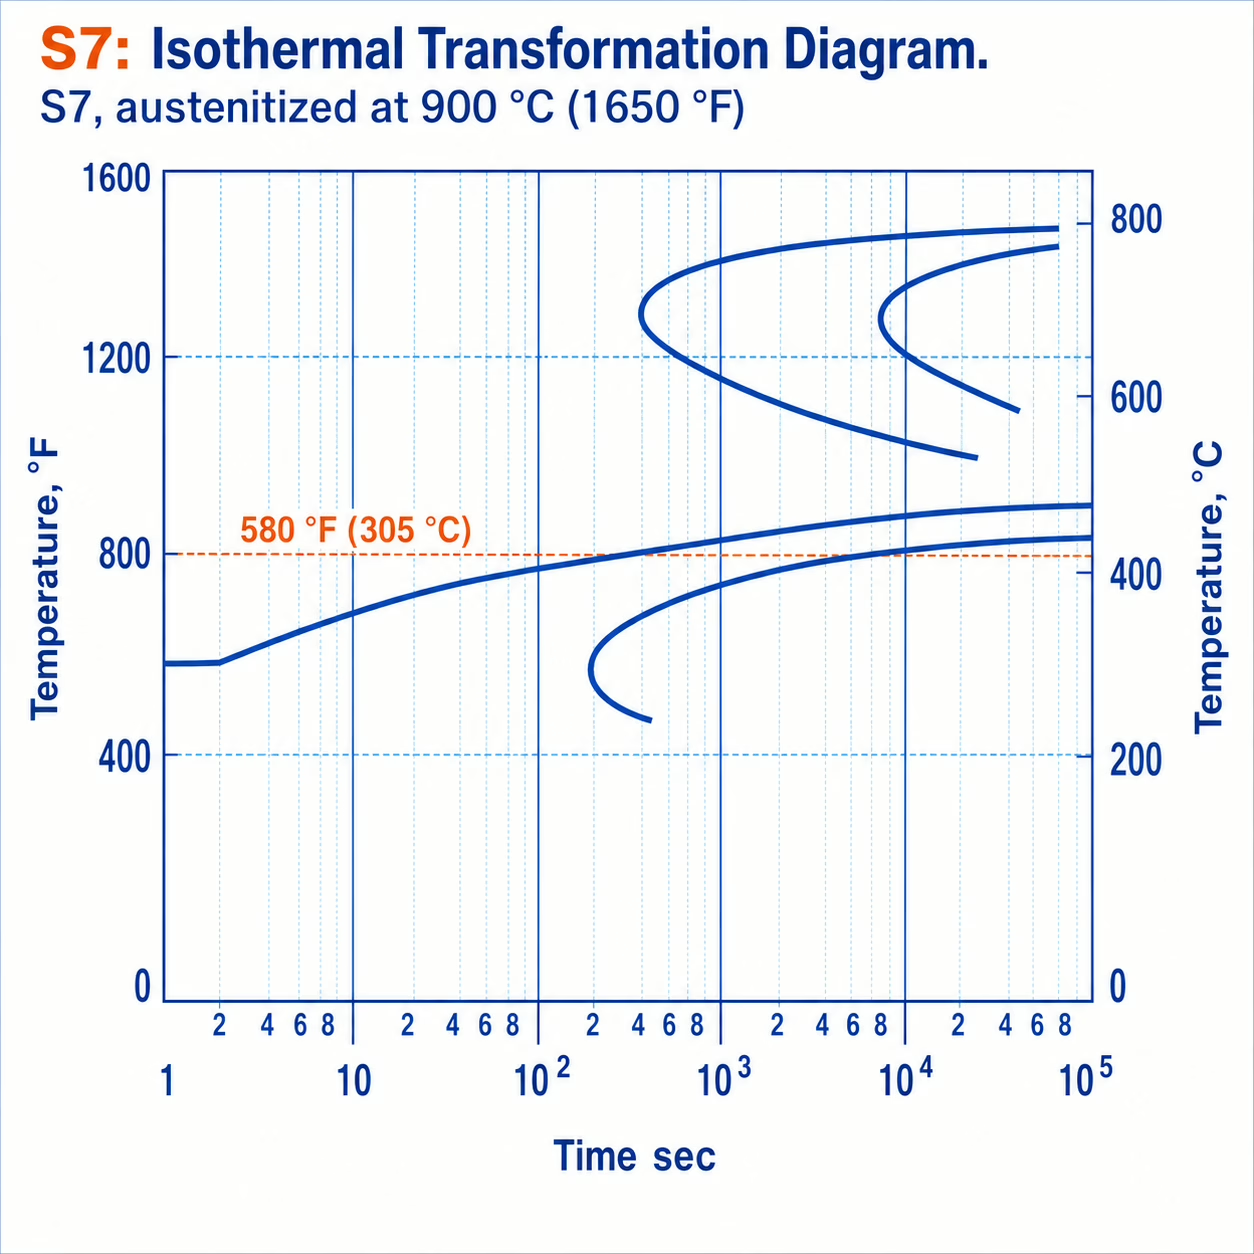
| Strength and toughness balance | Around 575 °F / 300 °C | Controlled hardness | Yield strength and impact balance |
For standard cold-work applications, 450 °F (about 230 °C) is commonly used to achieve stable hardness and good impact resistance.
For elevated-temperature service, the tempering temperature should normally be at least 25–50 °F above the expected service temperature. This helps prevent softening during use.
For shock-dominant tooling, higher tempering temperatures are often more suitable because toughness and fracture resistance are more important than maximum hardness.
S7 Tool Steel Quenching Method Selection
The correct quenching method depends mainly on section size, geometry, and distortion sensitivity.
| Condition | Method | Key Process | Critical Note |
|---|---|---|---|
| Sections ≤63.5 mm | Air quench | Cool in still air after austenitizing | Best dimensional stability |
| Sections >63.5 mm | Oil-based cooling | Use faster cooling to improve core hardness | Air cooling may be insufficient |
| Heavy sections requiring stress control | Flash oil quench | Oil quench until red heat disappears, then air cool | Do not use stainless steel foil |
| Complex or distortion-sensitive parts | Martempering | Salt bath at 595–650 °C, equalize, then air cool | Reduces thermal gradients |
For many S7 tools, air quenching is preferred because it reduces the risk of distortion. However, for large sections, air cooling alone may not provide sufficient cooling rate to achieve full hardness.
Common S7 Tool Steel Heat Treatment Problems
Most S7 heat treatment failures are linked to atmosphere control, section size, residual stress, excessive temperature, or delayed tempering.
| Problem | Root Cause | Corrective Action |
|---|---|---|
| Decarburization | Surface carbon loss in an oxidizing atmosphere | Use vacuum, controlled atmosphere, neutral salt, or sealed foil |
| Distortion or thermal cracking | Thermal gradients, sharp geometry, or machining stress | Preheat properly, stress relieve before hardening, avoid sharp corners |
| Low hardness in large sections | Cooling rate too slow through the section | Use oil-based cooling or flash oil quenching for heavier sections |
| Overheating or retained austenite | Excessive austenitizing temperature or soak time | Control temperature and soaking time strictly |
| Cracking after quenching | Delayed tempering or excessive internal stress | Temper immediately and apply double tempering |
Decarburization creates a soft surface layer that cannot fully harden, thereby reducing wear resistance. Overheating increases the risk of retained austenite, grain coarsening, dimensional instability, and lower toughness. Delayed tempering is especially dangerous because the as-quenched structure contains high internal stress.
Note: We do not provide S7 heat treatment services. Aobo Steel supplies S7 tool steel in the annealed condition, and this guide is provided as a technical reference to support our customers’ processing and application decisions.
Need S7 Tool Steel for Shock-Resistant Tooling?
Aobo Steel supplies S7 tool steel in annealed condition for industrial tooling applications. Send your required size, quantity, tolerance, and application for a quote.