
H13 Quenching Cooling Rates and Quench Media Chart
Cooling rates measured in H13 blocks and in die casting dies quenched with nitrogen, argon and helium in vacuum furnaces at 2 to 20 bar, set beside the average convective heat transfer coefficient of each quench medium. A reference summary of published practice and not an Aobo Steel specification.
Why the quench rate decides how an H13 die performs
Dies for aluminium die casting are usually machined close to final dimensions in the annealed condition and then heat treated in a vacuum furnace. Austenitizing takes place in the vacuum, and the die is cooled by admitting an inert gas into the chamber, with the gas jets arranged to impinge on the load. Pressure, velocity and volume of that gas together set how fast the die passes through the transformation range of H13, and those three variables are what a heat treater can actually adjust.
Cooling through the transformation range is the part of the cycle that decides how the die performs. Work published behind this report found that a relatively rapid rate improves toughness measured by the Charpy V notch test and improves thermal fatigue resistance measured from the cracking pattern of a purpose built thermal fatigue test. Where cooling is slow, the transformation of H13 produces pearlite and precipitates carbides on the prior austenite grain boundaries, and the die enters service with lower toughness and a shorter time to heat checking.
The working target used in the report is a cooling rate at the die face of at least 50 °F per minute over the 1750 to 550 °F interval, held in the first half inch below the working surface. The abstract of the same report states the goal as an average of more than 30 °F per minute half an inch below the working surface in premium grade H13 dies. Both figures are printed in the report, the stricter one being the rate at the face.
Quench media and their cooling power
How quickly a quenchant can pull heat out of a surface is expressed as a convective heat transfer coefficient, H. A higher coefficient means heat leaves the surface faster for the same temperature difference. The table below is the set of coefficients this report uses in its cooling models, from a vacuum with no gas movement at one end of the scale to a dilute polymer solution at the other.
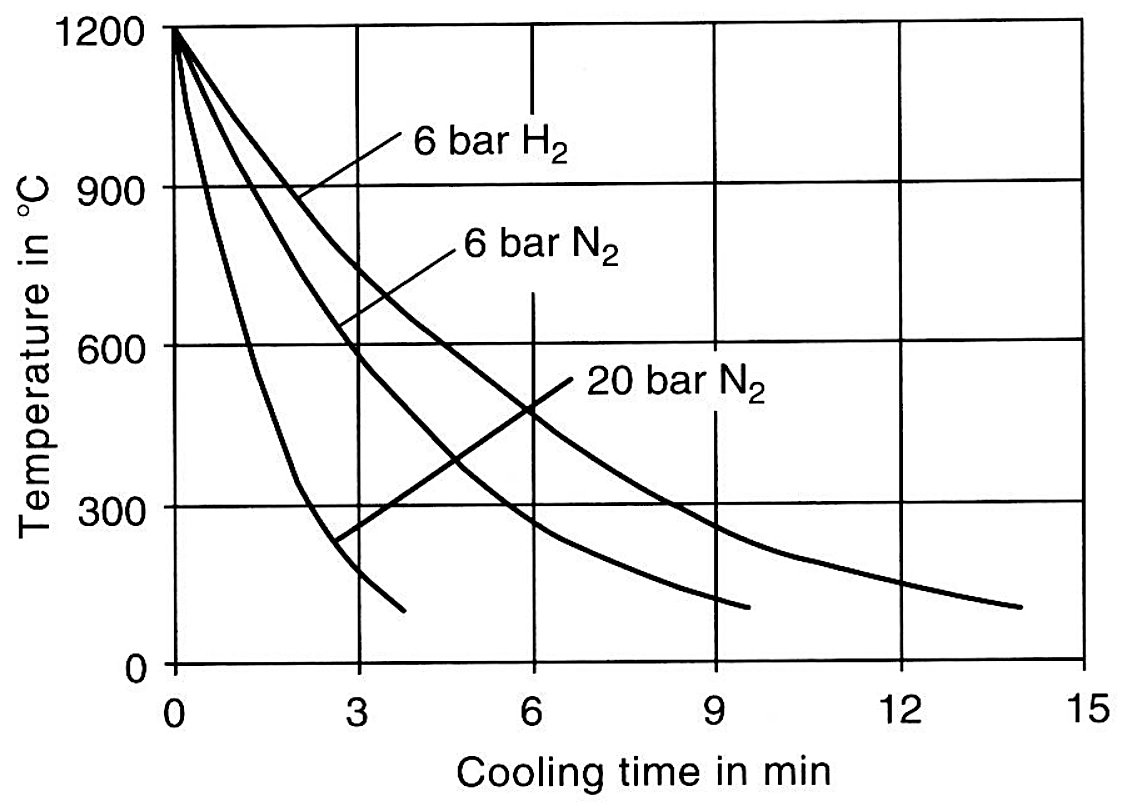
What those coefficients look like on an actual cooling curve, and how much agitation is worth, is measured on a standard probe below.
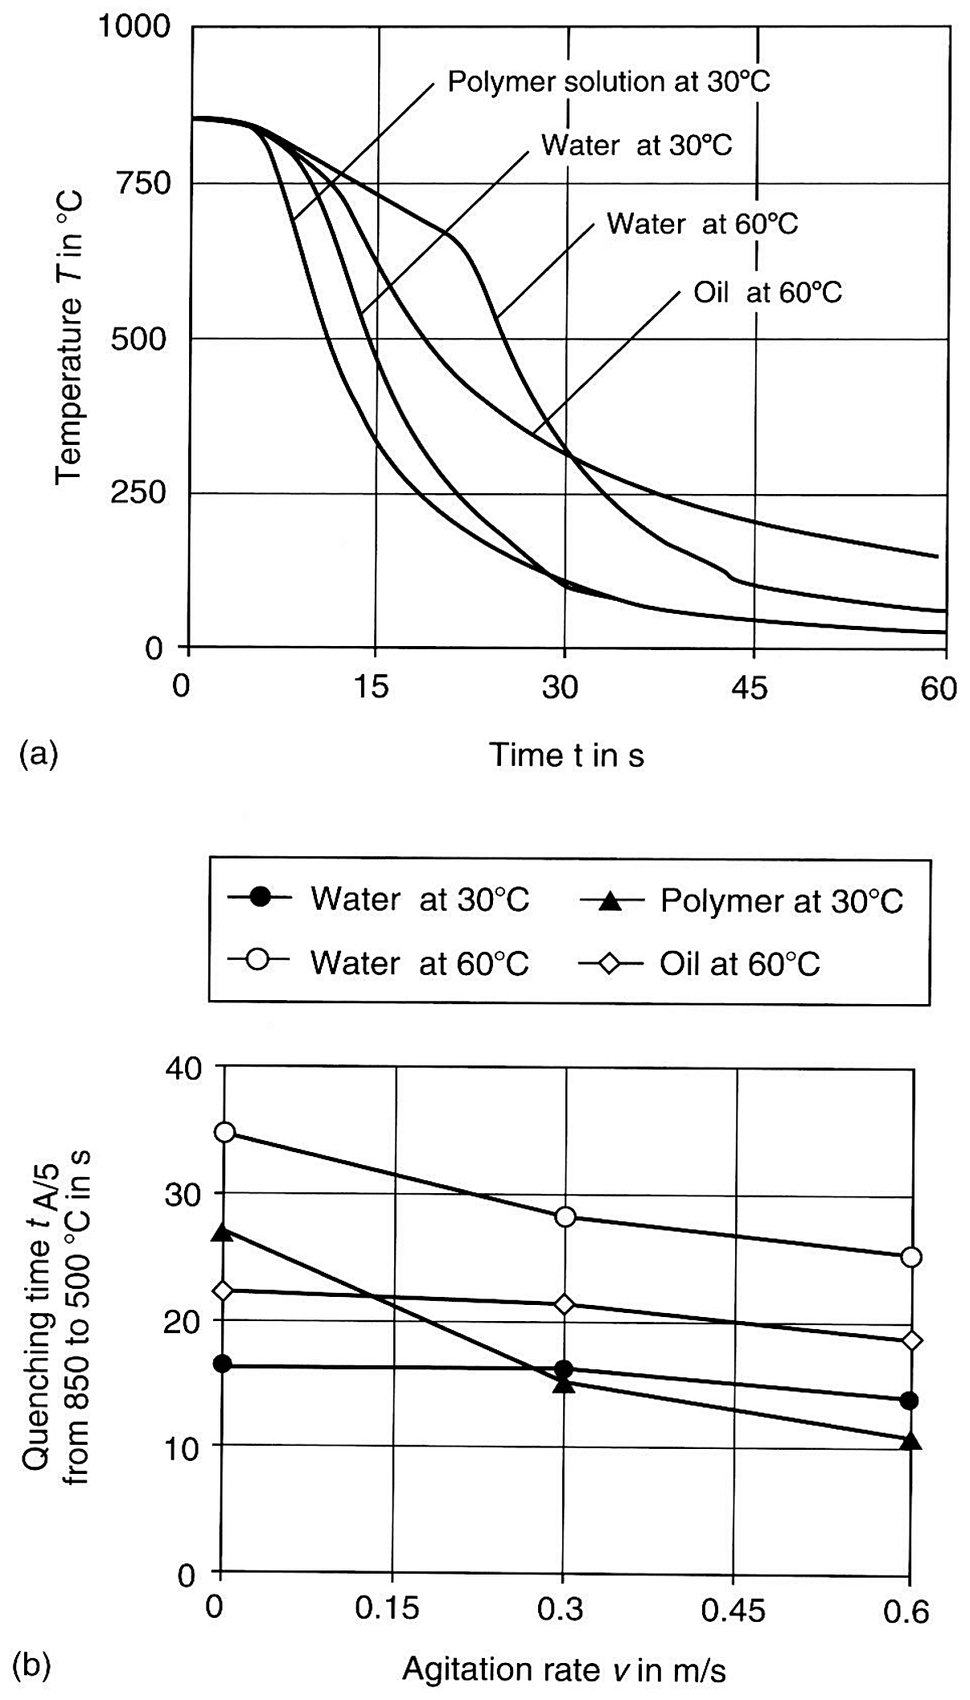
Average convective heat transfer coefficient by quench procedure
| Quench procedure | Average convective heat transfer coefficient, H (Btu/hr-ft²-°F) |
|---|---|
| Vacuum at 100 °F | 3.6 |
| Nitrogen at 100 °F, 2 atm. and 3,400 ft/min. | 13.9 |
| Helium at 100 °F, 2 atm. and 3,400 ft/min. | 19.2 |
| Low speed oil at 100 °F | 47.1 |
| Fluidized alumina at 100 °F | 61.7 |
| High speed rape/paraffin oil at 100 °F | 104.5 |
| Salt at 750 °F | 105.9 |
| Salt at 575 °F | 122.2 |
| 30% UCON A solution at 100 °F | 159.2 |
| 10% UCON A solution at 100 °F | 293.3 |
Source, average convective heat transfer coefficient determined for various quench procedures, Table I-4 of the report.
Gas quenching has no boiling stages, so its cooling power is set by the gas itself and the pressure it is held at.
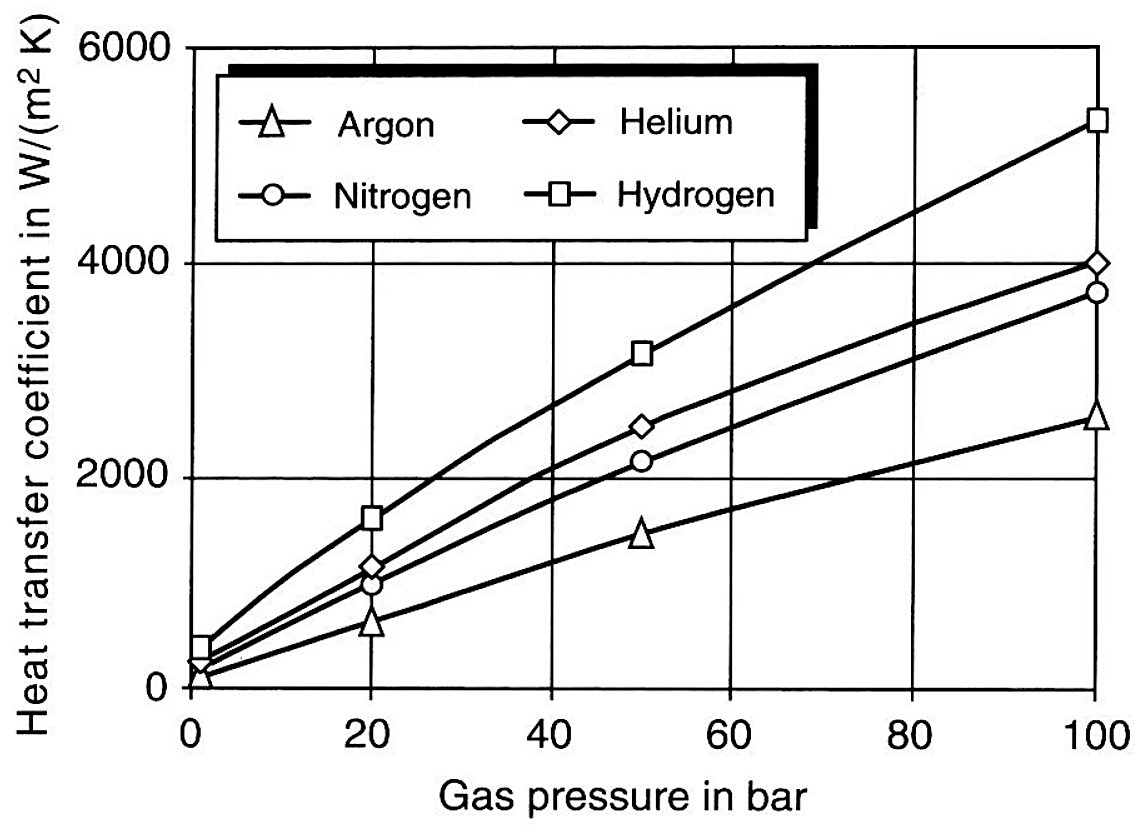
H is in Btu per hour per square foot per degree Fahrenheit. The salt entries are quoted at bath temperature and the remainder at 100 °F. The vacuum figure is radiation alone, which is the reason a vacuum furnace needs gas pressure and nozzle velocity before it can approach a salt bath. A coefficient describes the medium and the surface, not the part, so it cannot be read as the cooling rate of a die block. A reference table only, it is not an Aobo Steel recommendation.
The table gives an average for each procedure. Measured on a probe, the coefficient is not constant at all, and the shape of the curve is what decides whether the section misses the pearlite nose.
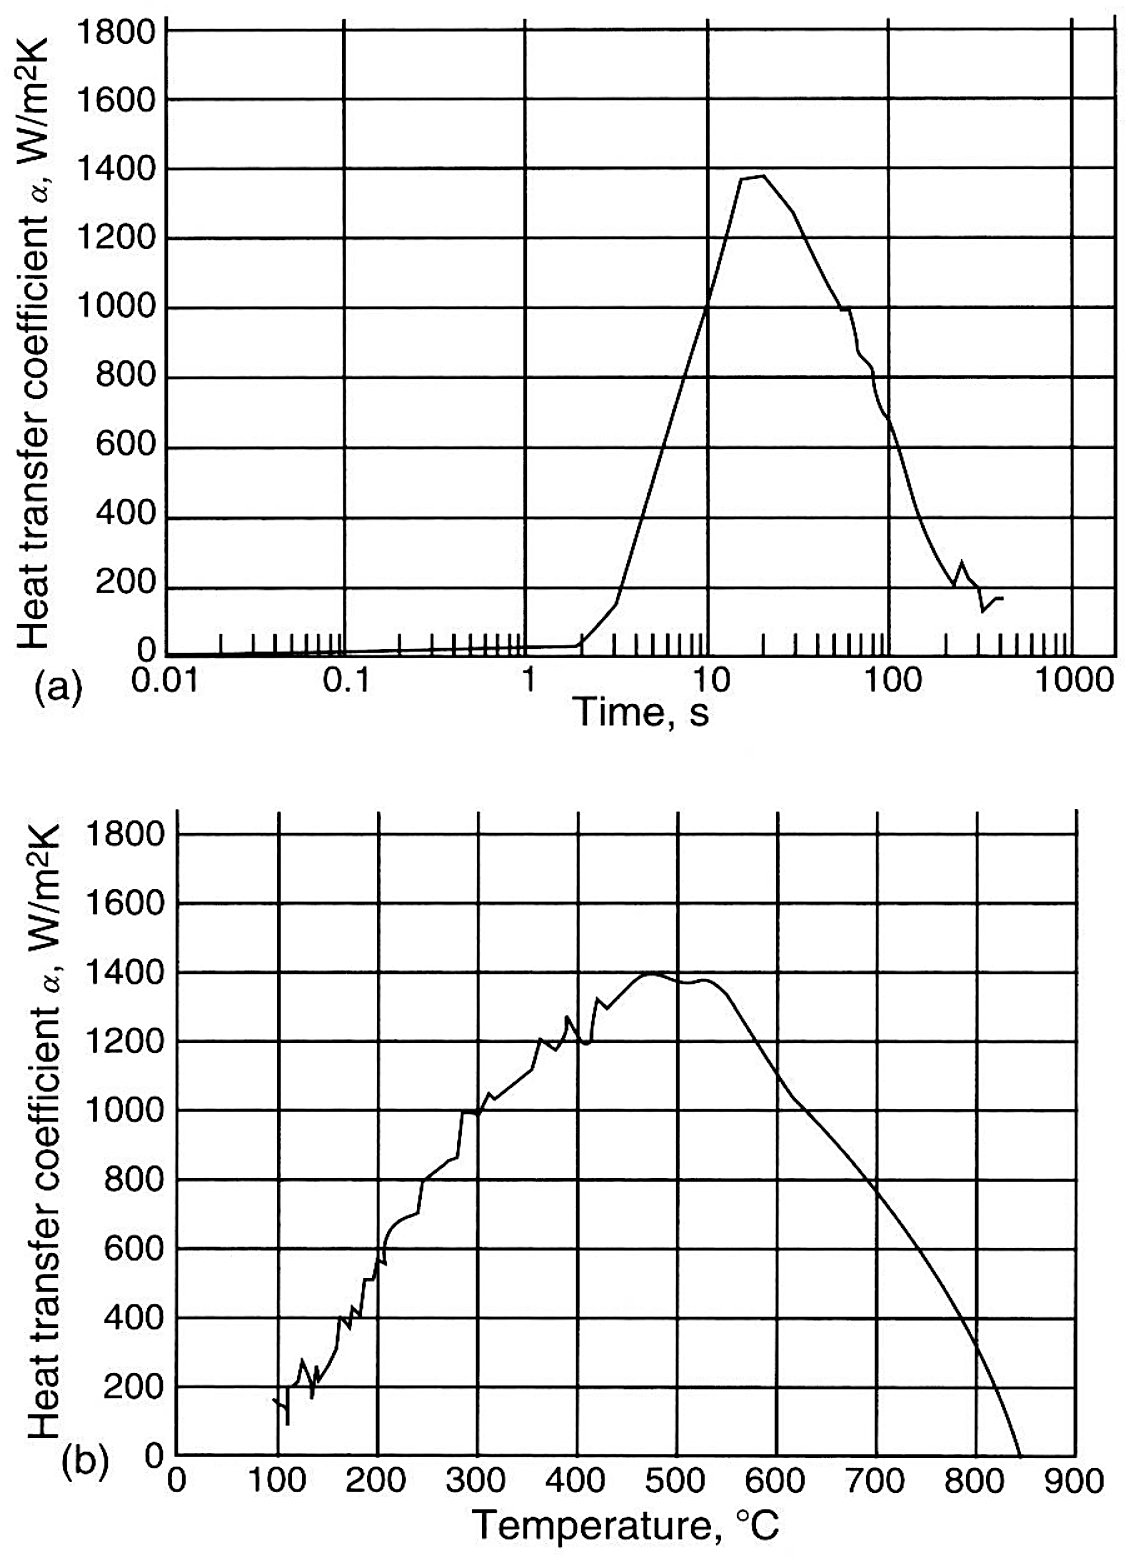
Cooling rates measured in H13 blocks and dies
The measurements below cover H13 blocks and production dies quenched in commercial vacuum furnaces, with one oil quench run as a baseline for both cooling rate and distortion. Nominal gas pressure is only one of the variables at work. The size and distribution of the gas nozzles, the power of the fan and the size of the furnace all move the result, and the fastest rate in this set came from the smallest furnace run at the highest pressure rather than from pressure on its own.
The gas curves for a tool steel bar, at two diameters, show how much of that theoretical range is left at the section sizes a die block actually has.
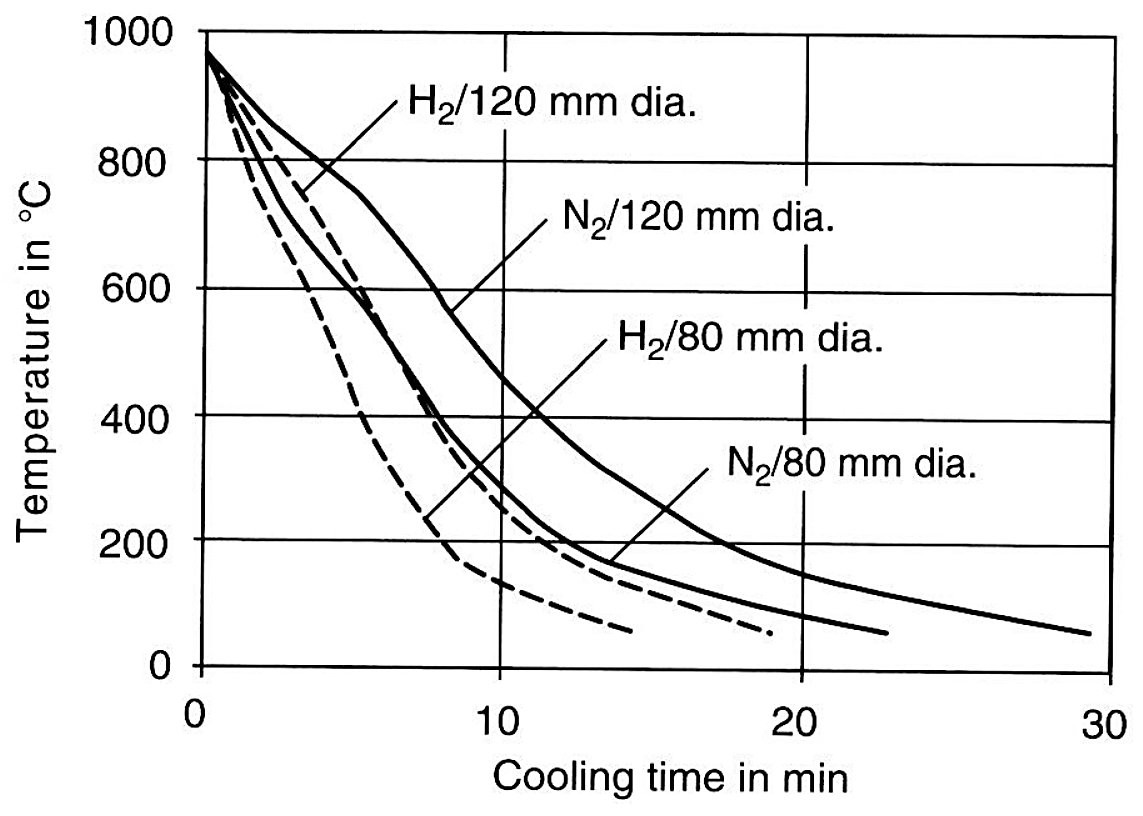
Surface and core cooling rates by furnace, pressure and medium
| Part | Heat treater | Furnace | Quench pressure | Quench medium | Surface cooling rate (°F/min) | Core cooling rate (°F/min) |
|---|---|---|---|---|---|---|
| Block #1 | Universal HT | Abar-Ipsen | 2 bar | Nitrogen | 39 | 30 |
| Die #2 | Universal HT | Abar-Ipsen | 2 bar | Nitrogen | 37 | 26.2 |
| Die #3 | IMP, London | Abar-Ipsen | 4 bar | Argon | 37.5 | 28.6 |
| Die #4 | FPM, Chicago | Abar-Ipsen | 5 bar | Nitrogen | 48 | 36 |
| Die #5 | FPM, Chicago | VFS | 7.5 bar | Nitrogen | 52 | 40 |
| Block #2 | FPM, Chicago | VFS | 10 bar | Nitrogen | 43 | 34 |
| Block #3 | FPM, Chicago | VFS | 10 bar | Nitrogen | 42 | 33 |
| Block #5 | Kowalski HT | Seco-Warwick | 20 bar | Nitrogen + helium | 126 | 62 |
| Block #6 | Euclid HT | Oil | oil | Oil | 120 | N/A |
Source, summary of quenching experiments, Table 7.1-36 of the report.
Cooling rates are in degrees Fahrenheit per minute, at the surface of the part and at its core. Reports of this work average the cooling rate over the 1750 to 550 °F interval, the range in which H13 transforms, and the table above does not repeat that interval. The source prints N/A where no core value was obtained, and the oil quench was run as a baseline for both cooling rate and distortion. The last row is printed in the source with Oil in the furnace column, oil in the pressure column and Oil in the quench medium column, and those three entries are reproduced here as printed. A reference table only, it is not an Aobo Steel recommendation.
Reading the two tables together
A coefficient and a cooling rate are not the same measurement. The coefficient belongs to the medium and to the surface. The cooling rate also depends on the section, because in a small part the convection at the surface is what limits the cycle, while in a thick die block the thermal conductivity of the steel becomes the limit and additional gas pressure then buys much less at the core than it does at the surface. That asymmetry is visible in the second table, where the 2 bar and 20 bar runs read 39 and 126 °F per minute at the surface and 30 and 62 °F per minute at the core.
Read against the 50 °F per minute face rate, the two runs at 2 bar and the 4 bar argon run sit below it at the surface, and the runs at 5 bar and above sit above it. Core rates across the set run from 26.2 to 62 °F per minute. The report’s own reading is that gas pressure alone does not settle the question, and that two furnaces run at the same nominal pressure are not a like for like comparison, so a quench that comes out slower than planned is usually traced to the furnace and its gas circuit rather than to the pressure setting alone.
Raising the pressure on a batch of cylinders does recover part of the gap between one gas and another, but not all of it.
H13 Quenching Cooling Rates and Quench Media Chart, printable PDF
Both tables on this page, the quench medium coefficients and the measured surface and core cooling rates for H13 blocks and dies, in one PDF with our contact details.
Related reference data
The grade this data belongs to is set out on the H13 tool steel page, with the rest of the cycle around the quench on the H13 heat treatment guide and the service hardness it has to reach on the H13 hardness chart. What happens when a quench goes wrong is covered on the quench cracking page, and the grades that harden in still air are separated from the rest on the air hardening tool steel page. Hardness held at working temperature is charted on the tool steel hot hardness chart, and the die casting side of the same grade is on the die casting die and insert page.
Source: Improved Life of Die Casting Dies of H13 Steel by Attaining Improved Mechanical Properties and Distortion Control During Heat Treatment (J. F. Wallace and D. Schwam, US Department of Energy final report DOE/ID/13320-3, October 1998).