
A2 Tool Steel Heat Treatment Guide
A2 tool steel is typically heat-treated by preheating to 1200-1250F (650-675C), austenitizing at 1750-1775F (955-970C), air quenching, and a double-tempering cycle at 400-450F (205-230C). Under controlled conditions, this process produces a stable working hardness of 58-62 HRC with a balanced combination of wear resistance, toughness, and dimensional stability.
A2 heat treatment controls hardness, wear resistance, toughness, and dimensional stability within a narrow processing window. As an air-hardening cold-work tool steel, A2 reduces quenching stress compared with oil- or water-hardening grades, but remains sensitive to temperature control, section size, and transformation behavior.
A2 Tool Steel Heat Treatment Process Quick Guide
| Step | Temperature | Time | Purpose |
|---|---|---|---|
| Preheating | 1200-1250F (650-675C) | Until equalized | Reduce thermal gradients |
| Austenitizing | 1750-1775F (955-970C) | ~1 hour per inch section | Form austenite |
| Quenching | Air to ~150F (65C) | – | Form martensite |
| First temper | 400-450F (205-230C) | 2 hours per inch | Relieve stress |
| Second temper | Slightly lower (~25F / 15C) | 2 hours per inch | Stabilize structure |
A2 heat treatment reference card, printable PDF
Two A4 pages with the quick parameter table, the tempering ranges, the step-by-step process, the hardness by stage and application, and the common problems. The PDF is in English.
Step-by-Step A2 Tool Steel Heat Treatment Process
1. Preheating
Preheat to 1200-1250F to ensure uniform temperature distribution and reduce internal stress before transformation. Insufficient preheating increases the risk of distortion and cracking.
2. Austenitizing
Austenitizing at 1750-1775F transforms the structure into austenite and partially dissolves alloy carbides. Holding time is based on section thickness, typically about one hour per inch after the part reaches full furnace temperature. Excessive temperature increases retained austenite and reduces hardness stability, while insufficient temperature leads to incomplete hardening.
3. Quenching
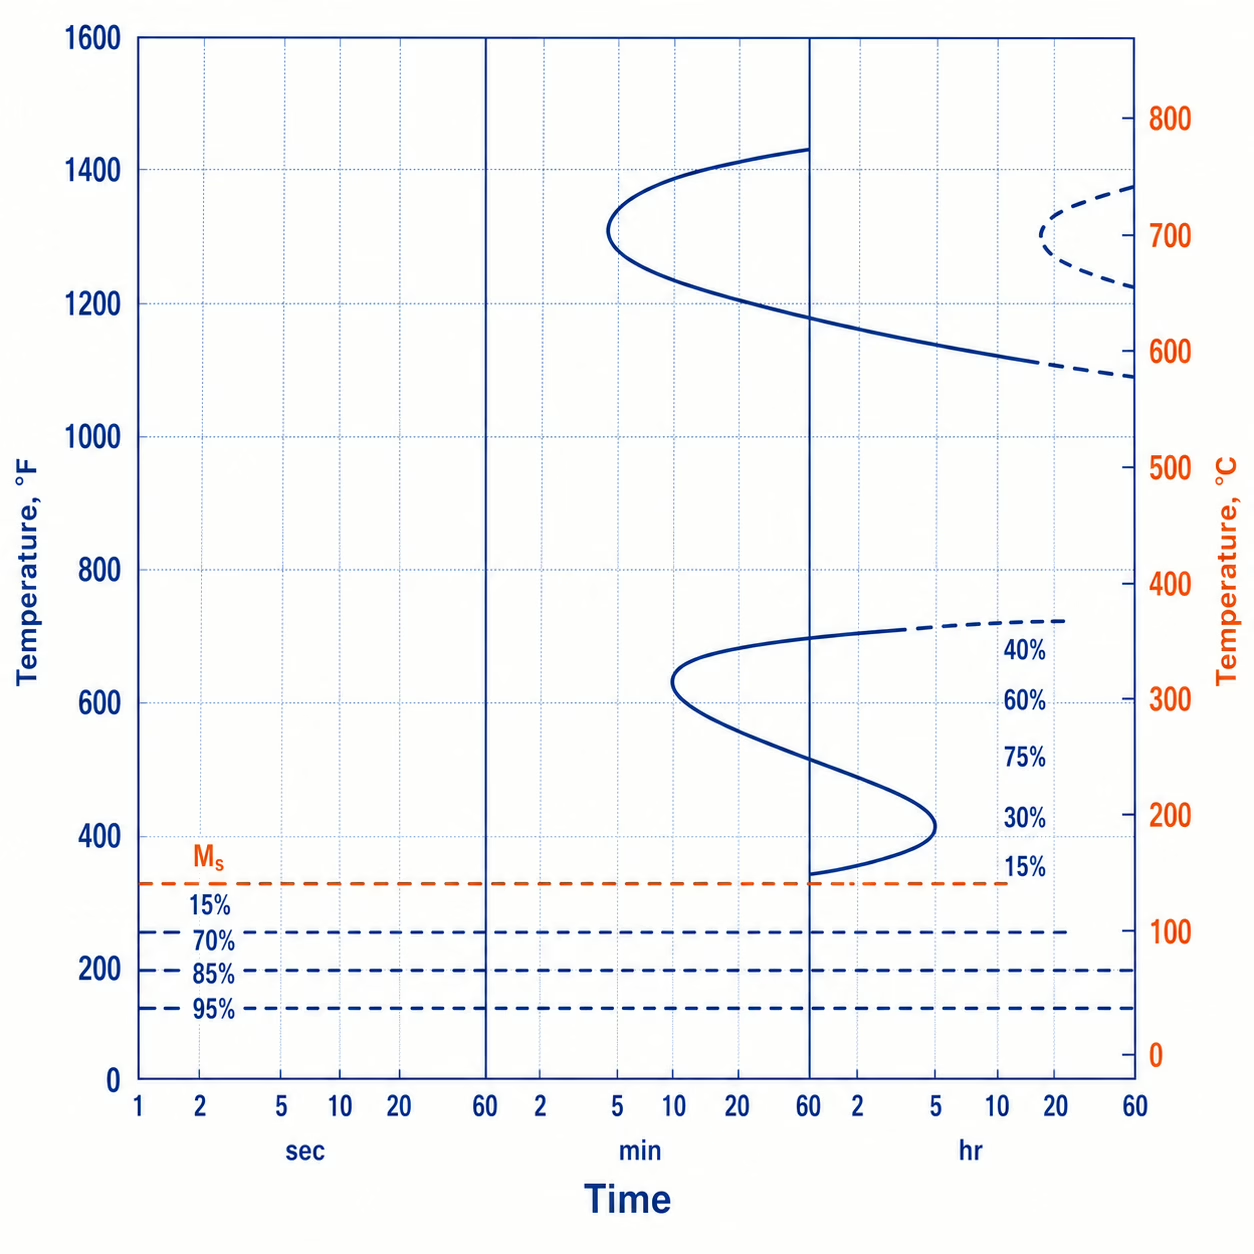
Quench in still air or a controlled gas. Cool the part to approximately 150F before tempering. For sections above about 5 inches (127 mm) in diameter, air cooling may not fully harden the core, and alternative cooling methods may be required.
4. Tempering
Tempering occurs immediately after quenching. The first temper at 400-450F reduces internal stress and adjusts hardness. After cooling, a second temper stabilizes the structure and prevents cracking during service.
5. Optional Subzero / Cryogenic Treatment
Subzero or cryogenic treatment may be applied after quenching to improve dimensional stability and consistency in hardness. This treatment transforms retained austenite into martensite and must always be followed by tempering.
A2 Tool Steel Hardness and Tempering
After quenching, A2 tool steel reaches an as-quenched hardness of approximately 64-65 HRC. The selected tempering temperature determines usable performance.
| Tempering Range | Typical Hardness | Practical Use |
|---|---|---|
| 250-400F (120-200C) | 60-63 HRC | Maximum wear resistance |
| 400-450F (205-230C) | 58-62 HRC | Standard cold-work applications |
| ~500F (260C) | Decreasing | Avoid (embrittlement risk) |
| 950-1000F (510-540C) | 56-57 HRC | Improved toughness and stability |
A2 Tool Steel Hardness After Heat Treatment
| Heat Treatment Stage | Typical Hardness | Practical Meaning |
|---|---|---|
| Annealed condition | 201-241 HB | Machining condition |
| As-quenched condition | 64-65 HRC | Not suitable for service |
| Standard tempered condition | 58-62 HRC | Typical working hardness |
| Tempered at ~400F (205C) | 60-61 HRC | Wear resistance focused |
| Tempered at 950-1000F (510-540C) | 53-57 HRC | Toughness focused |
| Cryogenic treatment + tempering | 61-62 HRC | Improved stability |
A2 is typically used in the tempered condition. Lower tempering temperatures favor wear resistance, while higher temperatures improve toughness and dimensional stability. The A2 tool steel hardness chart lists the full HRC range by condition and tempering temperature.
A2 Tool Steel Heat Treatment by Application
Select heat treatment for A2 tool steel based on the dominant failure mode rather than maximum hardness.
| Application Focus | Typical Tools | Heat Treatment Strategy | Resulting Hardness | Key Outcome |
|---|---|---|---|---|
| Maximum wear resistance | Blanking dies, shear blades, slitter knives | Low-temperature double temper (~400F / 205C) | 60-62 HRC | Maximum edge retention |
| Balanced wear and toughness | Punches, forming tools | Controlled tempering | 58-60 HRC | Reduced chipping |
| Maximum toughness | Impact-loaded tools | High-temperature temper | 56-58 HRC | Improved fracture resistance |
| Dimensional stability | Precision tools, gages | Cryogenic + tempering | 60-62 HRC | Stable size control |
| Surface wear resistance | Abrasive applications | Nitriding | Surface > core | Enhanced surface life |
Common Heat Treatment Problems and Solutions in A2 Tool Steel
| Problem | Root Cause | Practical Solution |
|---|---|---|
| Excessive retained austenite / unstable hardness | Overheating during austenitizing | Control temperature; apply cryogenic treatment if needed |
| Delayed cracking after quenching | Untempered martensite under high stress | Begin tempering at ~150F immediately |
| Embrittlement | Tempering near 500F (260C) | Avoid this range; apply double tempering |
| Surface softening or brittleness | Poor furnace atmosphere | Use controlled atmosphere; remove affected layer |
| Distortion or uneven hardness | Non-uniform heating or large section size | Proper preheating; controlled heating and cooling |
Stable A2 heat treatment depends on consistent temperature control, uniform heating, and proper sequencing of quenching and tempering. Stress relieving before hardening is recommended for precision parts, and controlled atmospheres are required to prevent surface degradation. Large sections require special attention to ensure uniform hardness distribution. Bar for these cycles is supplied annealed, turned and cut to length on the A2 tool steel round bar page.
A2 tool steel has limitations related to section size, temperature sensitivity, and stability. Large cross-sections may not fully harden in air, and austenitizing must be controlled within a narrow range. High-temperature surface reactions require controlled atmospheres, and improper tempering can reduce toughness or stability.